Hey everyone, I’m Jake, part of the team here at the Vickers Hardness Tester supply side, and I get this question literally every single week from new clients, lab managers, and even seasoned quality folks who’ve been using these testers for years: How often should I calibrate my Vickers hardness machine? It’s not a one-size-fits-all answer, and that’s what trips a lot of people up. I’ve seen guys who calibrate once a year no matter what, and others who calibrate every time they run a critical batch—both have their reasons, but neither’s always right. Let’s break this down like we chat over coffee, no stuffy jargon, just the real stuff I’ve picked up from 7 years of selling and supporting these machines. Vickers Hardness Testers
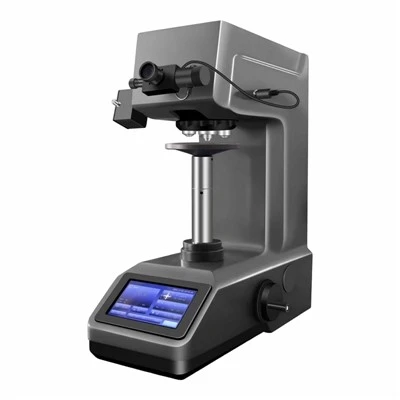
First off, let’s ground this in what calibration actually does, because a lot of people mix it up with maintenance. Calibration isn’t “fixing your machine”—it’s checking if it’s doing what it’s supposed to. A Vickers tester works by pressing a diamond pyramid into a sample with a set load, then measuring the diagonal of the indent to calculate hardness. If that load’s off by 10%, or the microscope’s measuring a diagonal that’s 5% longer than it actually is, your results are garbage. Calibration confirms those numbers are accurate against traceable standard blocks, right? So how often you need that check depends on three big things: how often you use the machine, what you’re testing, and how careful you are with it.
Let’s start with use frequency. If you’re a lab running 50+ tests a day, every single workday—say, a metal stamping plant testing parts for car seats that have to meet strict crash standards—your machine’s working hard. The load cell’s taking a beating, the diamond indenter can get tiny chips from hard samples, the microscope’s lens might get dust or smudges. For these heavy-use machines, we recommend quarterly calibrations. Wait, quarterly? That seems often, but think about it: I had a client last year making aerospace fasteners who thought once a year was enough. They had a batch of parts that tested too soft, but turns out the load cell had slipped 15% over 11 months, so all the results were off. They had to scrap $20k worth of parts—way more than the cost of four calibrations a year. Heavy use = more wear = faster drift.
Then there’s medium use: 10-15 tests a day, a few days a week—like a small machine shop testing tooling, or a research lab doing student projects. For these, semi-annual (twice a year) is standard. I’ve seen machines here that are 3 years old, used only a couple times a week, and their calibration’s still within spec because they don’t have the constant stress of heavy loads. The key here is consistency: if you use it the same amount every week, semi-annual works, but if you suddenly jump to 30 tests a day for a month, bump a calibration in there.
Light use is the wild card. If you’ve got a Vickers tester that’s tucked in the back closet, used only once a month for a random batch, or even just a backup machine—maybe annual calibration is okay, right? Wait, hold up. Even light use, I’ve seen machines that sat unused for 18 months and came out with load drift because the spring inside went stiff. Yeah, springs get stale when they’re not moving. So even if you only use it once a month, test it at least once a year, but if you haven’t used it in 6 months, do a quick pre-use check (we sell those little test blocks for $50, super easy) before you run your first real test. Don’t wait a year to find out it’s broken when you need it.
Next big factor: what you’re testing. This is where people make the biggest mistake. If you’re testing random samples in a research lab where results are just for a paper, once a year might cut it. But if you’re testing parts that have to pass FDA, ISO, or customer audits? Oh hell no. Most regulatory bodies (ISO 6506 is the main one for Vickers, by the way) require calibration to be traceable and documented, and the interval is usually dictated by your audit rules. I’ve got a medical device client who tests titanium implants for hip replacements—they calibrate their machine every month. Because if a hip implant is too soft, it breaks; too hard, it wears out too fast. The FDA doesn’t care if you do it every month, they care if your results are accurate. That’s non-negotiable. Same goes for aerospace parts, automotive safety components, any critical parts where a hardness failure means someone gets hurt. For non-critical stuff—like hobbyist metal projects, or testing aluminum cans where hardness only matters for bending strength—you can stretch it a bit, as long as you do a quick verification check every 3 months (not a full calibration, just a test on a standard block to make sure it’s close).
Then there’s machine handling and care. If you’re dragging your Vickers tester around the shop, knocking it into workbenches, not keeping it level (those things have to be perfectly level, by the way), or letting hard metal chips get stuck under the indenter—you need to calibrate more often. I had a client last quarter who ran their machine off a wobbly workbench, so every test was 8% off. They calibrated once a year, and that was the only reason they didn’t catch it sooner. If you’re gentle, keep the machine on a solid, level bench, clean the indenter after every test, then your interval can stay on the lower end. If you’re rough, bump it up by a quarter.
Wait, let’s talk about what’s not a calibration, because this is super confusing. A lot of people do a “check test” with a standard block every time they run a batch, and think that’s enough. It’s not. A check test is just a quick verification—if the result is within ±2% of the standard block’s value, you’re good, but if it’s off, you need a full calibration to find out why. That check test is a good middle step between full calibrations, especially for heavy use. We tell all our clients: full calibration every X months, plus a check test before any critical batch. That way, you catch small drifts before they turn into big mistakes.
Let me throw out some real examples from my clients to make this concrete. Last year, a custom tool and die shop called me panicking because their machine gave a result that was 10 points lower than the customer’s spec. They’d calibrated it 10 months prior, and thought it was fine. Turned out the indenter had a tiny crack (from testing super hard tool steel) that a 10-month-old calibration wouldn’t catch—calibrations check load and microscope, but not indenter condition every time. We fixed the indenter, did a new calibration, and found that the load had drifted 12% in those 10 months. If they’d calibrated twice a year, they would’ve caught the load drift and the indenter crack way earlier, and avoided a $15k rework bill.
Another example: a university materials science lab that only uses their machine for student lab experiments, 2-3 times a week. They were calibrating once a year, and that worked for years—until they had a new grad student who tested 10 samples in a row and got weird results. The lab director realized the microscope’s focus had slipped a tiny bit, and over the course of a year, that added up to a 7% error. They switched to semi-annual calibrations, and haven’t had a problem since.
What about new machines? If you just unboxed a Vickers tester for the first time, don’t wait. We recommend calibrating it within the first 30 days of use, even if you plan to do it again in 6 months. Manufacturing flaws are rare, but they do happen—we had a brand new machine go out where the load was off by 20% straight from the factory, and the only reason we caught it was the client did a first calibration. It’s a small step that saves you from dealing with bad results right out the gate.
Also, if your machine gets moved—even just across the shop to another bench—calibrate it after moving. Vickers machines are precision tools, and moving them can throw off the alignment of the load cell or the stage. I’ve seen guys move their machine on a Friday, run tests on Monday, and get all wrong numbers, because they skipped the post-move calibration. That’s an easy step, but it’s one people forget.
Now, let’s talk about the line in the sand where you should never skip a calibration. If your machine is used for 100% critical testing (audit, regulatory, aerospace, medical), quarterly is non-negotiable. If it’s for commercial testing (customer parts, general quality control), semi-annual is the minimum, even if you only use it a little. If it’s for research or non-critical hobby stuff, annual is okay, but only if you do that pre-use check every time you fire it up.
Wait, I should also mention what calibration entails, because some people think it’s just a $100 block test. A proper calibration for a Vickers tester includes checking the applied load against standard weights, measuring the indenter’s angle (the diamond pyramid has to be exactly 136 degrees, if it’s off even a degree your results are wrong), checking the microscope’s magnification and the indent measurement accuracy, and verifying everything against NIST-traceable standard blocks. That’s not a quick test—take a few hours, but it’s worth every penny. A lot of people try to do it themselves with a cheap block, but unless you have access to a micro-hardness tester and traceable weights, you’re not doing a real calibration. That’s where we come in—we don’t just sell testers, we sell calibration services too, so you can get that proper traceable check done without hunting for a third party.
Let’s wrap this up with a quick cheat sheet, because I know you don’t want to re-read all this to find the answer.
- Heavy use (50+ tests/day, 5 days/week, critical parts): Calibrate every 3 months + pre-critical batch check.
- Medium use (10-20 tests/day, 2-4 days/week, commercial QC): Calibrate every 6 months + pre-batch check.
- Light use (<10 tests/week, non-critical): Calibrate every 12 months + pre-use check before any major test.
- Any time you move the machine, drop it, or notice weird results: Do a calibration right away, no matter when the last one was.
And before you ask—no, there’s no magic number that works for every machine. I’ve had a machine that ran 80 tests a day for 2 years and still only needed semi-annual calibrations, because the owner kept it level and clean. I’ve had a machine that ran 10 tests a week and needed quarterly calibrations because it was banged around. It’s all about your specific setup.

If you’re still stuck, or you’re trying to figure out what interval makes sense for your lab or shop, hit us up. We’ll walk you through your use case, your testing needs, and make a recommendation that’s not too frequent (so you don’t waste money) and not too infrequent (so you don’t have bad results). No hard sells, just honest advice, since that’s how we’ve been doing this for years. We know how much a wrong hardness test can cost you—whether it’s rework, scrap, or even a recall—and we want you to have the right info to avoid that.
Metallographic Consumables References
ISO 6506-1:2014, Metallic materials — Hardness test — Brinell, Vickers and Vickers pyramid hardness — Part 1: Test method
ASTM E384-22, Standard Test Method for Microindentation Hardness of Materials
National Institute of Standards and Technology (NIST) Handbook 150, Calibration Policy and Requirements for Measurement and Test Equipment
Laizhou Metallographic Testing Equipment Co., Ltd.
As one of the leading manufacturers and suppliers of vickers hardness testers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to wholesale customized equipment at competitive price from our factory. Welcome to contact us for quotation.
Address: TENG GE PO ZI VILLAGE, HU TOU YA TOWN, LAIZHOU CITY, YANTAI SHANDONG, CHINA
E-mail: nicolecheng@lzmetaltest.com
WebSite: https://www.metalnesscn.com/
